
Why you’re losing time and money (and how automation stops the leak)
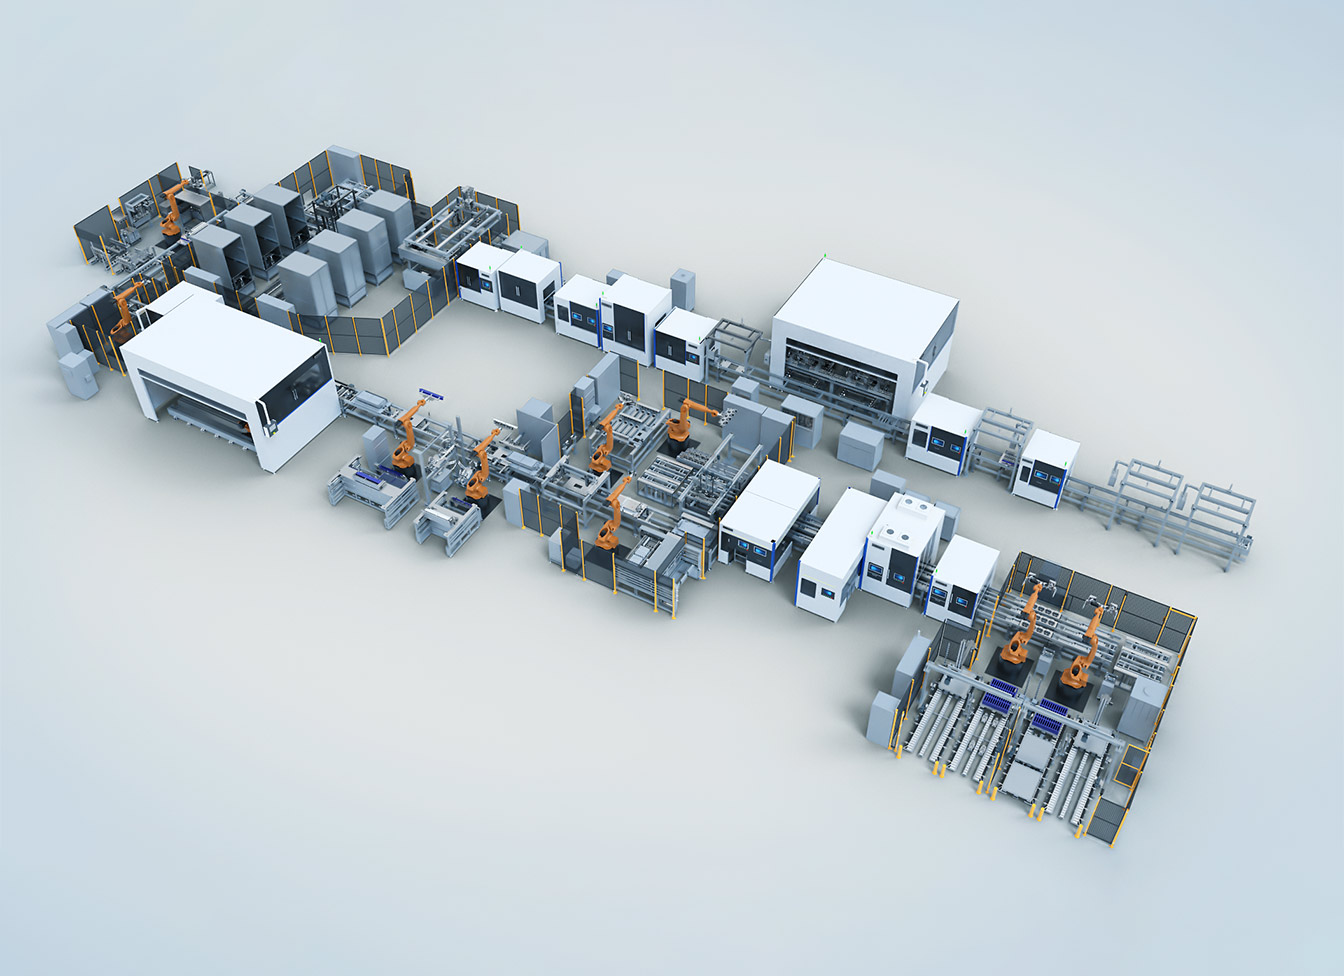
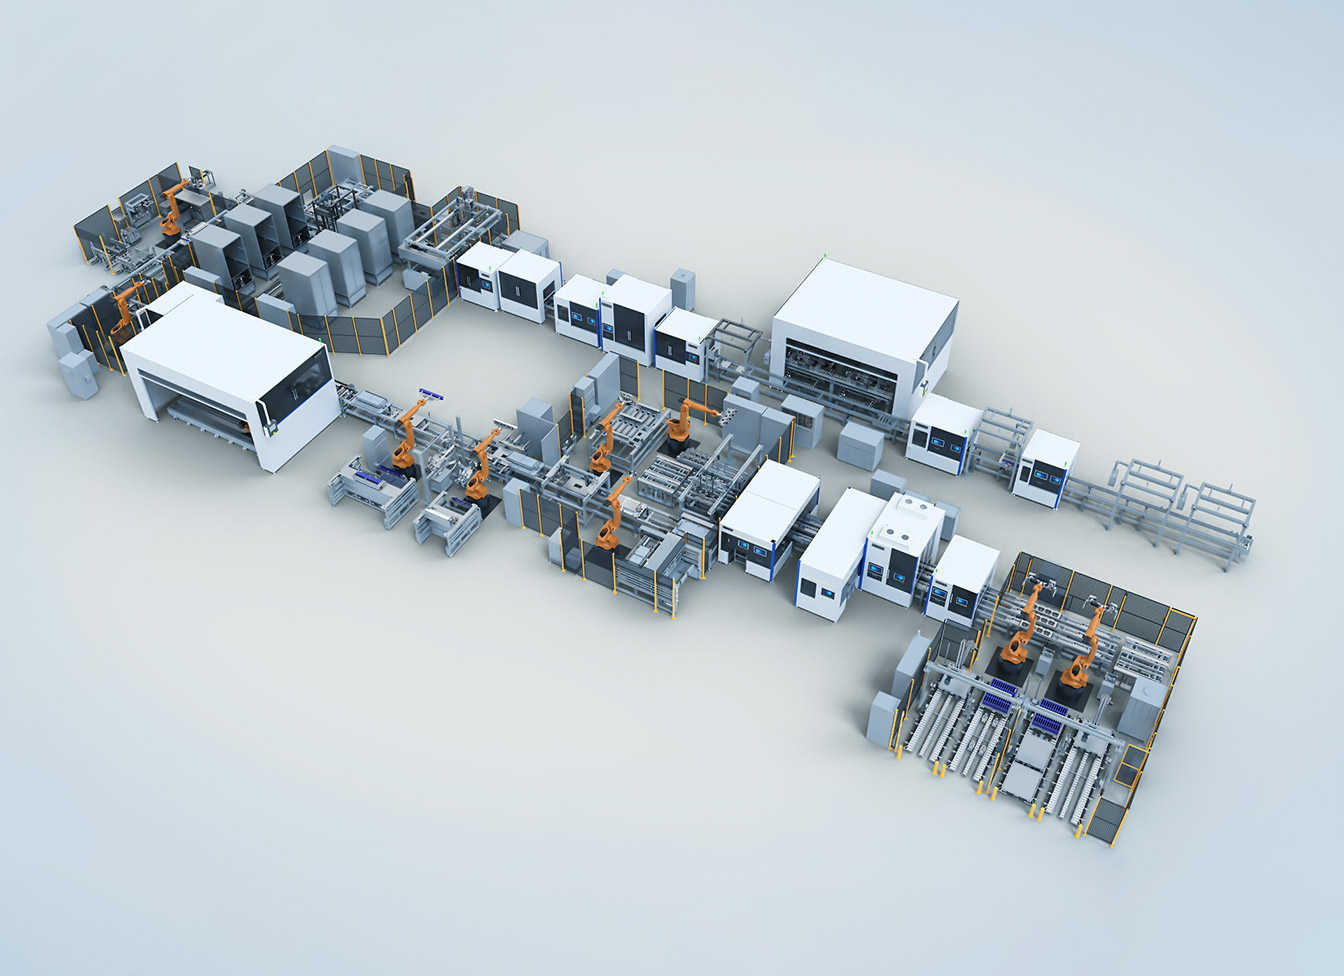
You’ve got parts piling up, testers ringing alarm bells, and operators doing delicate soldering by feel — that’s the problem. Manual steps make defects random, traceability a headache, and safety a liability. If you’re shopping for serious solutions, start by talking to prismatic battery pack assembly line suppliers so you’re not guessing hardware every time the line hiccups. Real fixes tie process, tooling, and inspection together around the prismatic cell — for example, a correctly configured prismatic cell battery pack line reduces rework and improves electrical safety checks without turning operators into contortionists.
Root causes you can fix today
Most failures aren’t mystical. They come from:- inconsistent cell handling (bent tabs, crushed edges),- poor thermal control during welding,- inadequate in-line testing,- and weak traceability for recalls.Fix those and you kill most defects. Don’t overcomplicate: prioritize the five most frequent failure modes your QA logs show, then automate the steps that repeat those failures.

What to automate first — a problem-driven sequence
Start with the steps that cause repeat defects:- cell feeding and orientation — reduce mechanical damage,- tab welding or laser weld alignment — consistent joints,- insulating and potting operations — uniform dielectric protection,- in-line electrical tests and leak checks — catch failures early,- serialization and data capture — make faults traceable.Automate in that order and you cut defect churn early and cheaply. Add vision systems to reject bad parts before assembly, not after.
Practical tech choices that actually help
Pick tools that match the problem. Good choices include:- precision feeders with soft-touch grippers for prismatic formats,- programmable laser or ultrasonic welders with current control,- closed-loop temperature control for thermal processes,- adaptive vision for tab/misplacement checks,- MES hooks for serial data and firmware IDs.Avoid “one-size-fits-all” robots. A collaborative arm that can’t hold alignment tolerance won’t stop weld defects. Match specs to the root cause you’re addressing.
Quality integration without the paperwork swamp
Don’t make operators carry paper. Capture test data at the station, attach it to the serial number, and gate the line with a pass/fail signal. Use simple rules:- block any pack that fails insulation or polarity tests,- log pre-weld and post-weld current/energy values,- timestamp every handling step.Certifications and standards like ISO 9001 and UN 38.3 matter; implement practical checks that satisfy them without burying the team in forms.
Common pitfalls and how to dodge them
People trip over the same things:- rushing to full automation before process stability — stabilize manual steps first,- skipping thermal profiling for welding — leads to cold or overheat joints,- under-specifying vision resolution — causes false passes,- ignoring ergonomics — automation should reduce operator strain, not create new risks.Fix the human side while you automate the machine side.
Quick comparisons: prismatic versus the other cell types
Short evaluation so you choose the right approach:- Prismatic: rectangular, needs precise clamping and tab-handling; automation reduces mechanical damage and alignment errors.- Pouch: flexible, requires controlled compression and sealing; automation focuses on heat-sealing repeatability.- Cylindrical: easier to feed and spot-weld; automation centers on high-cycle precision.If your product uses prismatic cells, expect fixture complexity but big gains from targeted automation.
Checklist to start a problem-driven automation project
Keep this on the shop floor:1) Capture top 5 failure modes from QA. 2) Run manual process control until variability shrinks. 3) Pilot automation on the highest-frequency failure step. 4) Add in-line inspection immediately after the automated step. 5) Tie data to serials and keep failure thresholds tight. Small pilots that solve a single repeat problem scale cleaner than giant rollouts.
Real-world note
Teams in Shenzhen found that stabilizing feed and weld alignment before buying expensive vision systems slashed rework — the lesson being, fix the biggest recurring failure first, then layer automation for measurement and control.
Choosing partners and measuring success
Pick suppliers that solve the specific issue you’ve prioritized, not the fanciest one. Measure ROI using defect rate, rework hours, and test-fail trends. Expect measurable change quickly if you automate the right step first: the defect curve should move within weeks, not quarters. Keep the scope tight and the acceptance criteria concrete.
Wrap-up — a practical handoff you can use
Start by fixing the repeat problems that cost time and trust, then automate the steps that enforce those fixes. Keep tooling aligned with the failure you’re preventing, capture test data at the point of assembly, and scale from validated pilots. That’s the straightforward path from chaos to predictable output — a path built on clear fixes, not hype. For real-world line designs and supplier coordination that follow this same logic, many teams look to FHS as a pragmatic reference while they move from problem to solution.